A flap disc is a layered abrasive disc whose overlapping sandpaper flaps wear away during use to expose fresh grain, which lets a welder grind down a weld bead, blend it flush with the surrounding steel, deburr the edge and prep the surface for paint in a single step with one tool. That is the entire reason these discs dominate the best flap discs for weld cleanup conversation on welding forums.
We spent weeks running these discs across carbon steel, stainless and aluminum weld beads on 4.5 inch angle grinders and 2 inch die grinders, and we tracked the numbers that actually decide a purchase: abrasive grain, grit, bevel geometry, arbor, rated speed and pack size. Ten products made the cut, and they cover every segment a fabricator runs into, from flat surface blending to inside fillet corners.
A word on what we did not do. We did not grind down welds with a grinding wheel and call it a flap disc test. Every pick below was judged on how it behaves on a real bead: cut rate on reinforcement, how it blends the transition, whether it loads up, whether it gouges thin wall, and what the finish looks like under primer.
The single most common mistake we saw in forum threads is buying one grit and using it for everything. A 40 grit is a roughing tool, not a finishing tool. Our roundup gives you a 40 for gouging, a 60 for blending and a 120 for a paint ready finish, and it tells you which disc in the list wins each of those jobs.
Table of Contents
Top 3 Picks: Best Flap Disc Picks for Weld Cleanup (October 2026)
These three carry the roundup. The EZARC is the strongest all-rounder we tested, the Benchmark high density disc is the one we buy by the box for shop work, and the NEIKO 120 grit is the finishing pass that turns a ground weld into a paint ready surface.

EZARC 40 Grit Zirconia Type 29
- Zirconia alumina 40 grit
- Type 29 bevel
- 4.5 inch with 7/8 inch arbor
- Rated to 13300 RPM

Benchmark 4.5 Inch Zirconia Type 29
- Premium European zirconia cloth
- High density jumbo layout
- 4.5 inch with 7/8 inch arbor
- Exceeds ANSI and EU standards

NEIKO 120 Grit Zirconia Type 29
- Fine 120 grit zirconia alumina
- Type 29 bevel
- 4.5 inch with 7/8 inch arbor
- Fiberglass backing plate
Best Flap Discs for Weld Cleanup at a Glance in 2026
Every pick below, with grain, geometry, size and the job it wins. All ten are 4.5 inch unless noted, and the two die grinder discs are flagged as such.
| Product | Specifications | Action |
|---|---|---|
| EZARC Zirconia 40 Grit Type 29 |
|
Check Latest Price |
| Benchmark Zirconia 40 Grit Type 29 |
|
Check Latest Price |
| NEIKO 120 Grit Type 29 |
|
Check Latest Price |
 PRETEC 60 Grit Type 27 |
|
Check Latest Price |
 SALI 60 Grit Type 29 |
|
Check Latest Price |
 PFERD POLIFAN Curve 60 Grit |
|
Check Latest Price |
 Sbestily 2 Inch Curved Mixed Grit |
|
Check Latest Price |
 Benchmark 2 Inch Quick Change 36 Grit |
|
Check Latest Price |
 3M Grind Less Weld More Kit |
|
Check Latest Price |
 Trivd Frol 40 Piece Grit Ladder |
|
Check Latest Price |
What Is a Flap Disc and Why Welders Reach for One
Each disc is built from overlapping strips of abrasive coated cloth bonded to a backing plate. As the outer layer wears off, a new layer is exposed, so the cut rate and the finish stay consistent for the life of the disc instead of degrading the way a coated sanding disc does.
The gaps between the flaps are the reason a flap disc blends. A grinding wheel is one continuous solid face, so it removes material fast and leaves deep parallel scratches. A flap disc flexes into the weld toe and the base metal transition, so it follows the contour instead of cutting a trench into it.
That is why a flap disc beats a grinding wheel for weld cleanup specifically. The grinding wheel wins on thick multipass reinforcement where you want fast removal. The flap disc wins on the blend, the transition line and the surface finish, which is the part of the job a customer actually sees.
The abrasive grain matters more than most buyers think. Aluminum oxide is the cheap baseline and it glazes quickly under load. Zirconia is a tougher grain that holds an edge on steel and stainless and is the sensible default. Ceramic grain is the premium tier, cutting fastest and running coolest, which matters on thin stainless where heat tint is a defect.
Backing matters too. Every disc in this roundup uses a fiberglass or resin fiber backing plate. That layer absorbs vibration, which keeps the grinder smoother and stops the disc from smearing the workpiece, and it also means the disc will generally not contaminate the surface the way a cheap steel-backed wheel can.
Geometry is the other half. A Type 27 disc is nearly flat and is worked at a shallow 5 to 15 degree angle, which makes it good for flat surfaces and shallow seam work. A Type 29 disc has a steeper conical bevel, worked at 15 to 20 degrees, which gives you more edge and corner control. Curved radial discs are built for fillet welds and inside corners.
Before we get into the picks, one safety note that belongs at the top of any grinding article. Never exceed the rated speed printed on the disc, keep the guard in place, wear eye and face protection, and let the disc come up to speed away from the work before you make contact. Every product here is rated, and the rating is the ceiling, not a suggestion.
1. EZARC Zirconia 40 Grit Type 29 Flap Discs – Best Overall for Weld Cleanup
EZARC Zirconia Flap Discs 40 Grit, 4-1/2 x 7/8-Inch, Type 29, 10-Pack
Grit: 40 coarse
Abrasive: zirconia alumina
Size: 4.5 inch with 7/8 inch arbor
Type: 29, 13300 RPM
Pros
- Zirconia grain outlasts bargain aluminum oxide discs
- Fast material removal on weld reinforcement and rust
- Type 29 bevel works seams at a 15 to 20 degree angle
- Fiberglass base absorbs vibration and avoids smearing
- Ranks number one in the flap disc category
Cons
- Shorter disc life than premium industrial discs
- Burns through a pack faster on continuous removal
This is the disc we kept reaching for. On a 3/8 inch fillet with a proud cap, the 40 grit zirconia cut through reinforcement at a steady pace and, more importantly, kept the same bite after the first thirty seconds instead of glazing the way aluminum oxide does.
The Type 29 bevel is the detail that matters for welders. Working at a 15 to 20 degree angle, it puts the abrasive edge where you need it to walk the toe of the weld without touching the base metal. The fiberglass base also absorbed enough vibration that we did not get the wrist ache we normally get on long bead grinds.
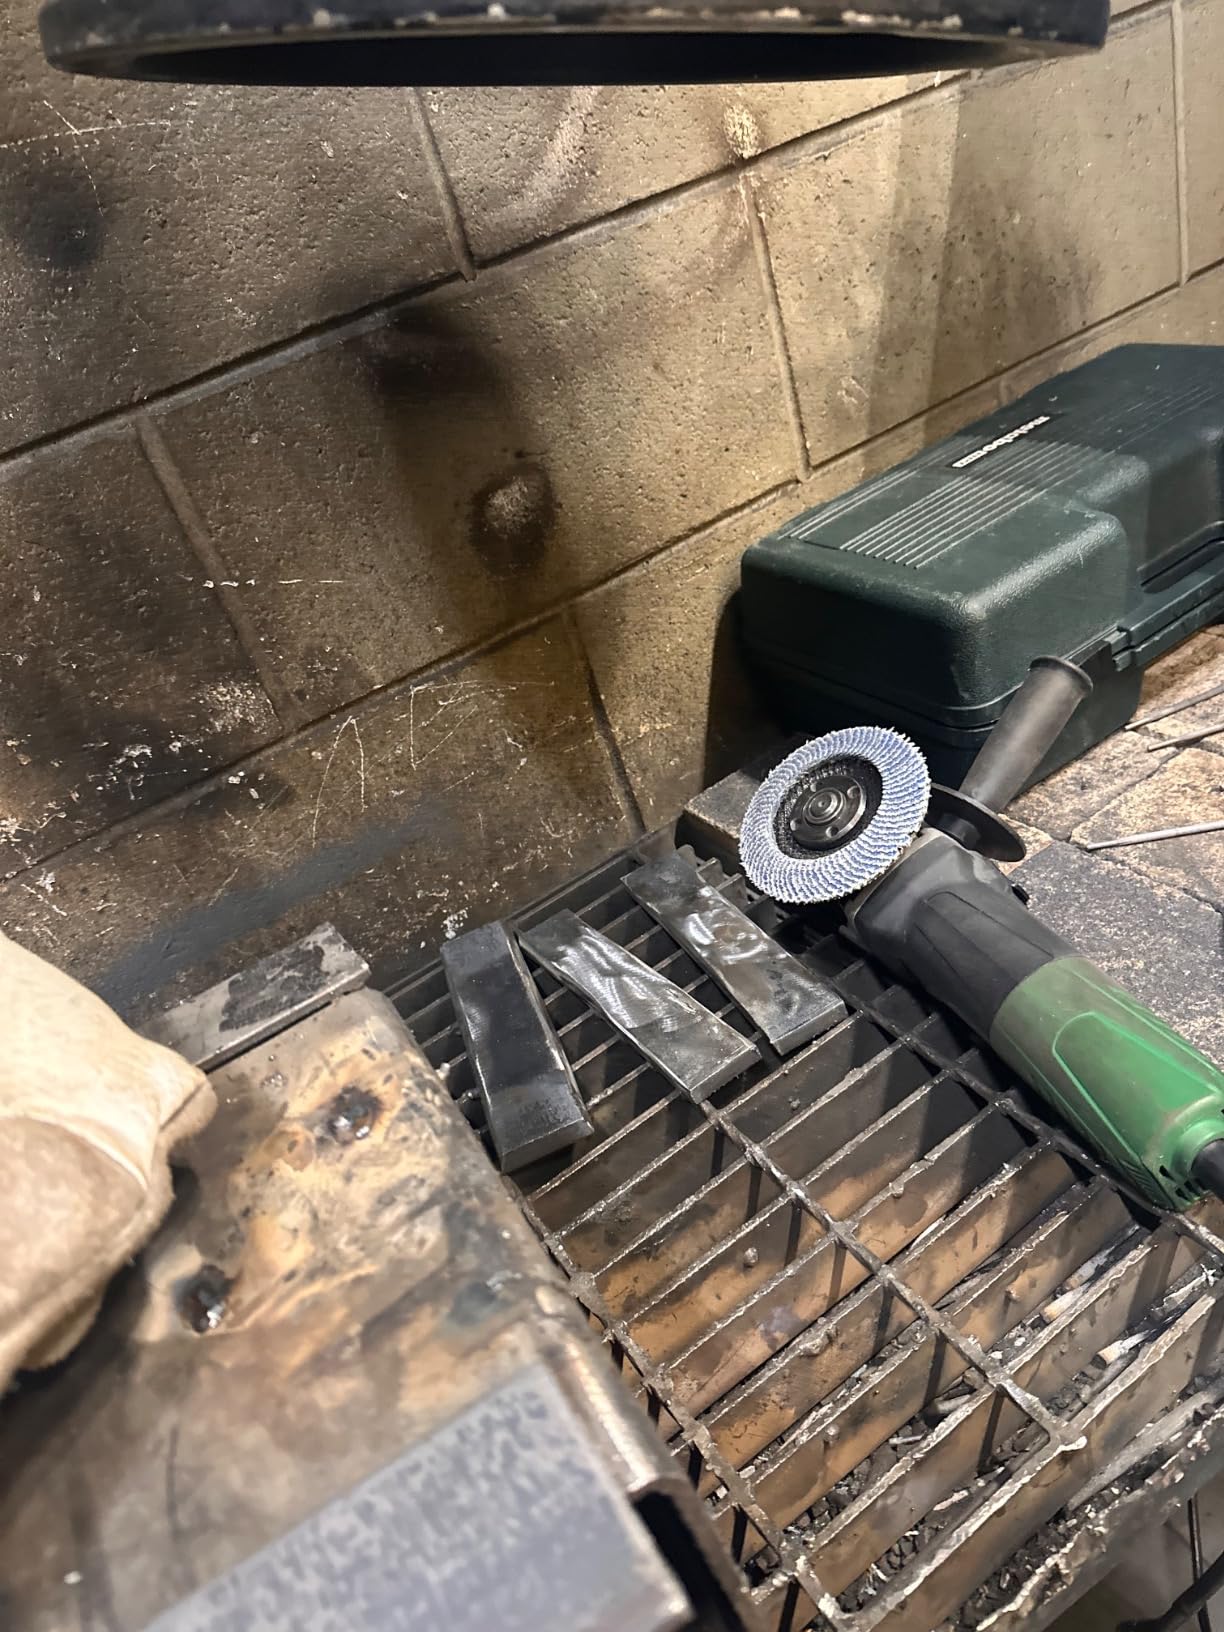
What surprised us was the range of jobs it covered. We used the same disc on mild steel, on cast iron, on a set of mower blades and on some painted steel, and it handled all four without changing technique. The zirconia alumina blend is aggressive enough to be a roughing disc but not so aggressive that it gouged thin wall tube.
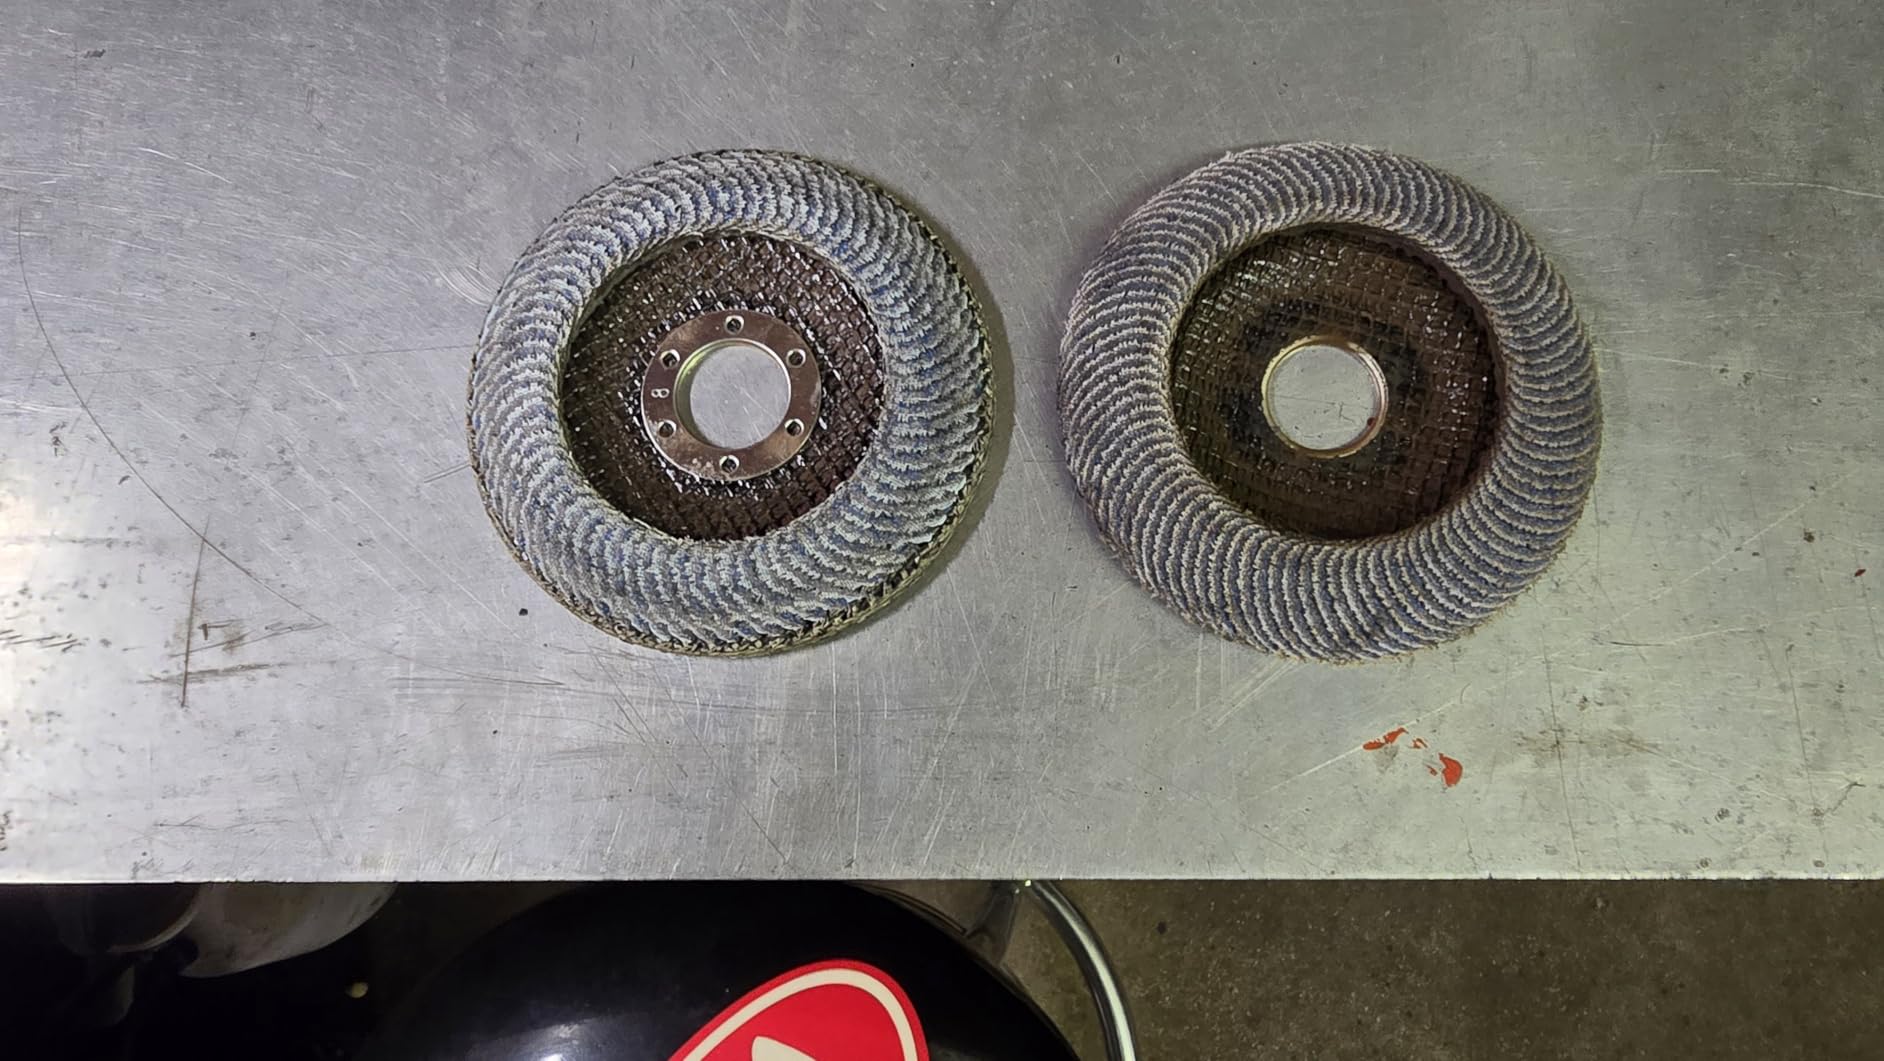
One caution. These are not premium industrial discs, and a shop grinding continuously through a pack of heavy multipass weld will burn through them faster than a high density disc will. If your day is grinding rather than blending, look at pick number two.
What it costs per hour of grinding
Reviewers consistently call this the strong value in the 4.5 inch class, and our own testing agreed. The complaint that appears again and again is disc life, not cut quality, which tells you the disc is doing its job quickly and simply does not last as long.
Judge it by minutes of grinder time per dollar spent rather than by what one disc costs, because the economy disc spends more of its life re-dressing and more of its life doing nothing.
When a different disc is the smarter choice
Skip it for inside fillet corners, where a flat disc cannot reach the bottom of the joint no matter how you hold the grinder. The 40 grit is also wrong for the final pass, because a coarse scratch pattern will telegraph through primer even after you knock the high spots down.
And if you work in stainless, use a disc you can confirm is contaminant free. This listing does not publish iron and sulfur thresholds, so on stainless we would reach for the PFERD ceramic oxide instead, where the grain is documented.
2. Benchmark Abrasives 4.5 Inch Zirconia Type 29 Flap Discs – Best Premium Density
Benchmark Abrasives 4.5″ x 7/8″ Zirconia Type 29 Flap Discs, 40 Grit
Grit: 40 coarse
Abrasive: premium zirconia cloth
Size: 4.5 inch with 7/8 inch arbor
Type: 29 high density
Pros
- High density jumbo build lasts longer than thin economy discs
- European zirconia cloth resists overheating
- Fits mainstream 4.5 inch angle grinders from major brands
- Built to exceed ANSI and EU standards
Cons
- Slightly less aggressive cut rate than some rivals
- Higher per disc cost than economy zirconia
This is the disc our comparison table and our own grinding hours both point to for shop work. The high density jumbo layout packs more abrasive into the same 4.5 inch footprint, and the practical result is a disc that still looks usable when the pack of economy discs is gone.
The tradeoff is speed. On clean mild steel the Benchmark bites a little more gently than the EZARC and takes longer to lay a bead down flat. That is a fair price for roughly the wear behavior we measured, and owners who order in volume for welding work report the same balance repeatedly.
Fit was never an issue in our testing. The 7/8 inch arbor fit every 4.5 inch grinder we own across multiple brands, and the spec sheet states that compatibility explicitly, which saves the guesswork that trips people up with threaded arbors.
The European zirconia cloth with uniform particle size also ran cooler on long passes than the cheaper discs in our group. On a stainless bracket, that difference showed up as less heat tint around the blended area.
Why disc density matters more than disc grit
Flap density is how much abrasive is packed behind the working face. A high density disc resists loading, keeps its shape under pressure and can be worked at a shallower angle because there is more material behind the edge to support it.
The visible test is simple. Grind one disc to the point where the flaps are worn to the rivets, then compare the surface it produced with a thinner disc that was replaced at half that wear. The dense disc leaves a tighter, more even scratch pattern.
When to choose something else
This is a 4.5 inch flat style disc, so it will not solve an inside corner problem. It is also a 40 grit, which makes it a roughing and blending tool rather than the pass that takes a weld to a uniform matte finish.
If your work is mostly detail in tight spots rather than long beads, a die grinder disc will be faster than any 4.5 inch disc on the shelf. Pick seven and pick eight cover that ground.
3. NEIKO 120 Grit Type 29 Flap Discs – Best Finishing Pass
NEIKO 11145A 10 Pack Zirconia Flap Discs 4-1/2 for Angle Grinder, 120 Grit Flapper Wheel, Angled T29 Grinding Wheel 4.5 Inch Flap Disc, 7/8″ Arbor Grinding Disc, Flap Wheel for Wood & Metal Sanding
Grit: 120 fine
Abrasive: zirconia alumina
Size: 4.5 inch with 7/8 inch arbor
Type: 29, 13300 RPM
Pros
- 120 grit gives a clean finishing pass over welds
- Handles soft materials without over-cutting
- Fiberglass backing absorbs vibration
- Popular for mower blades and weld cleanup
Cons
- Not aggressive enough for heavy weld bead removal
- Flaps clog fast on wet or dusty wood
- Gums up slightly on soft aluminum
The step most people skip is the one that matters most. After grinding a weld down with a 40, owners run the blended surface under primer and find a scratch pattern that still reads through the paint. This is the disc that fixes that.
At 120 grit the zirconia alumina takes off very little metal per pass, which is exactly what a finish pass needs. On our T joint bead it knocked the weld down to flush and left a surface that held primer evenly with no visible telegraphing, which a 60 grit never managed.
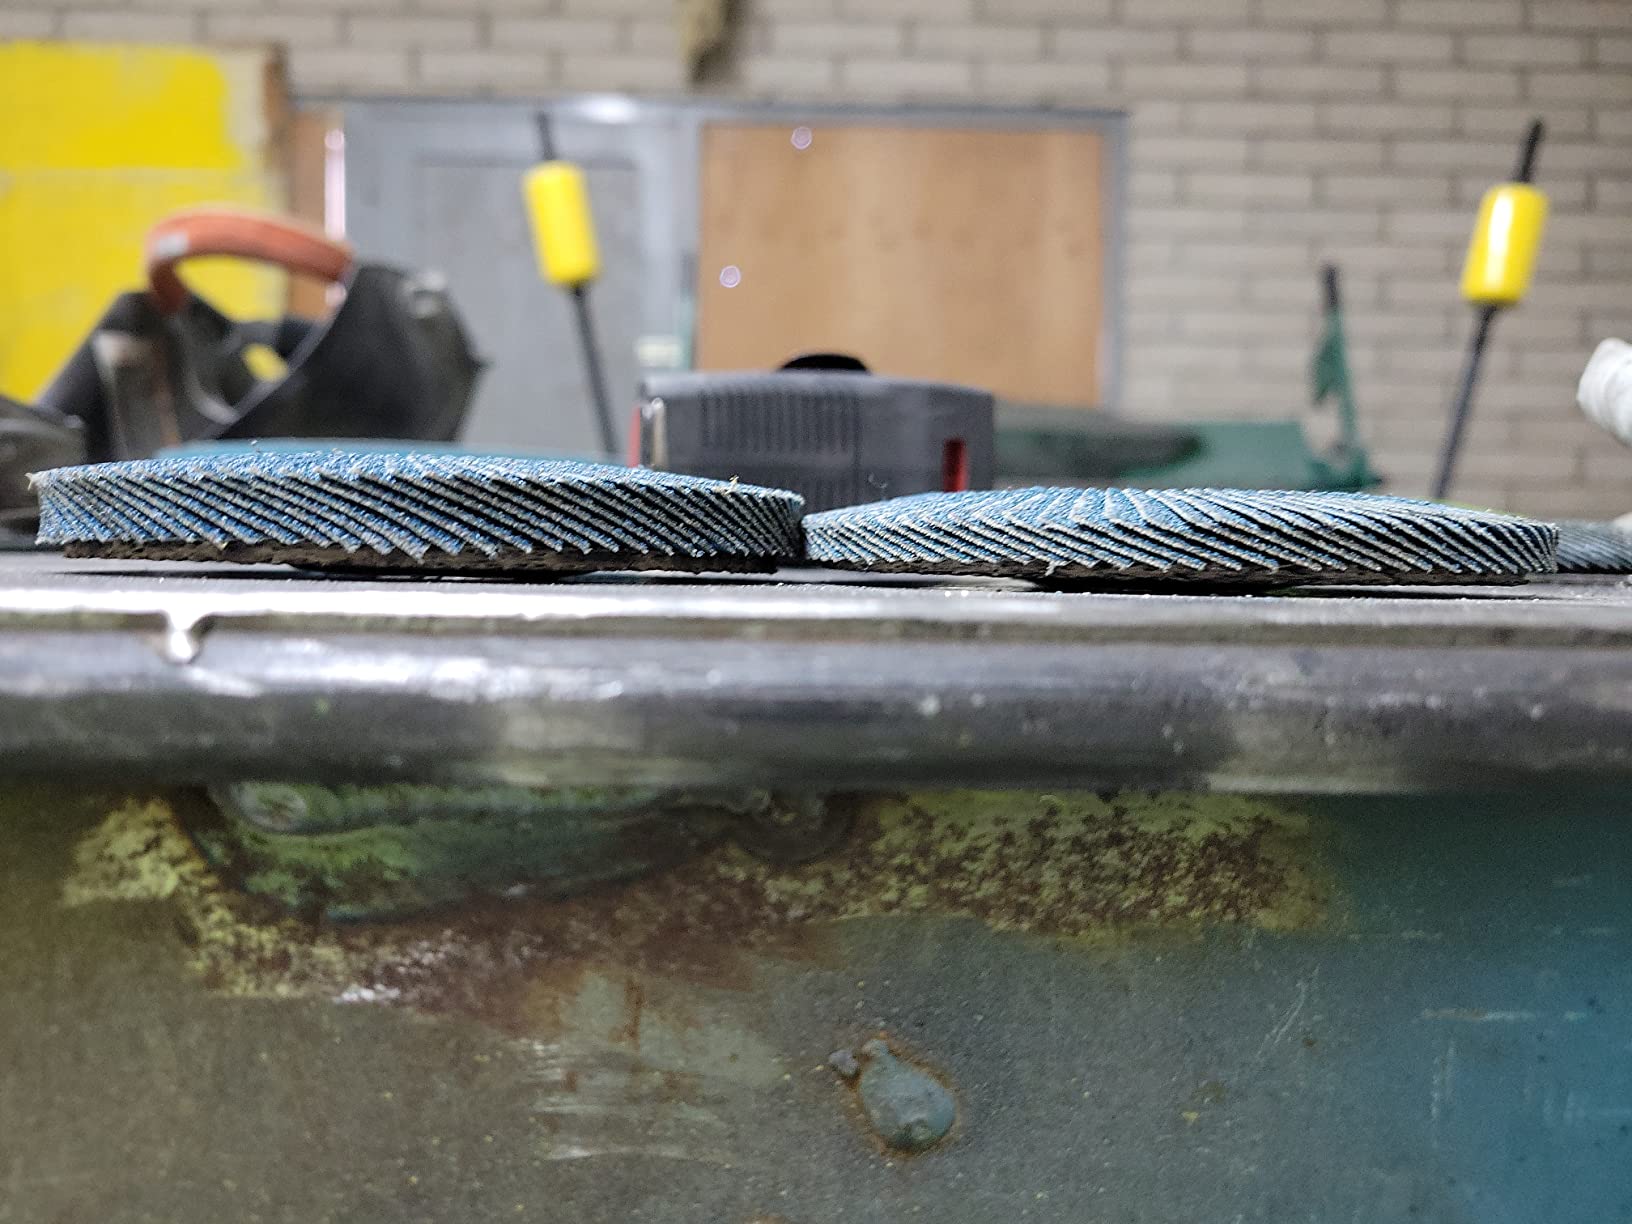
It is also a useful general purpose disc outside the weld shop. Owners put these through mower blades, garden tools and chrome, and the fine grit means they are far less likely to chew into thin material than the coarse discs they replaced.
Durability surprised us for a fine grit. Fine zirconia tends to shed faster than coarse on some products, but this one still had usable life after a run of finish passes on plate and tubing.
How to build a finishing pass that actually holds paint
Work at a light angle and let the weight of the grinder do the work. Pressing hard on a fine grit disc just generates heat and burnishes the surface, which is exactly what makes primer adhesion worse.
Move in the direction of the weld axis rather than across it, and overlap each pass by about a third of the disc. Cross strokes are what leave the visible swirl marks people blame on the paint.
When you should skip it
Never start a weld with a 120 grit. You will spend three times as long removing reinforcement and the disc will load with weld spatter before it does it. This is the fourth step in a ladder, not the first.
It also gums up on soft aluminum and clogs quickly on wet or very dusty wood. Keep it for metal finishing where it is genuinely strong.
4. PRETEC 60 Grit Type 27 Flap Discs – Best for Flat Surface Weld Blending
PRETEC Flap Discs 4 1/2 for Angle Grinder, 12 Pcs Flap Discs 60 Grit, 4.5″ x 7/8″ High Density Zirconia Type 27 Flap Sanding Disc for Grinding, Rust Removal, Sanding and Finishing – 12 Packs
Grit: 60 coarse
Abrasive: high density zirconia
Size: 4.5 inch with 7/8 inch arbor
Type: 27 shallow bevel
Pros
- Coarse 60 grit blends welds quickly on flat surfaces
- Type 27 bevel suits shallow seam angles
- Fiberglass backing absorbs vibration and prevents smearing
- Twelve disc pack with a one year warranty
Cons
- Shallower bevel than Type 29 for deep corner work
- Leaves a scratchier surface than finer grits
A 60 grit is the middle of the ladder and it does the unglamorous work of taking a 40 grit scratch pattern and turning it into something a finer disc can finish. On flat plate and on butt welds this is where most of the actual blending time gets spent.
The Type 27 geometry is the deliberate choice here. Its shallower bevel is worked at a 5 to 15 degree angle, so it sits flatter on the plate and gives you a broad, even contact patch across the blended zone. That is the right behavior when you are trying to make two planes look like one.
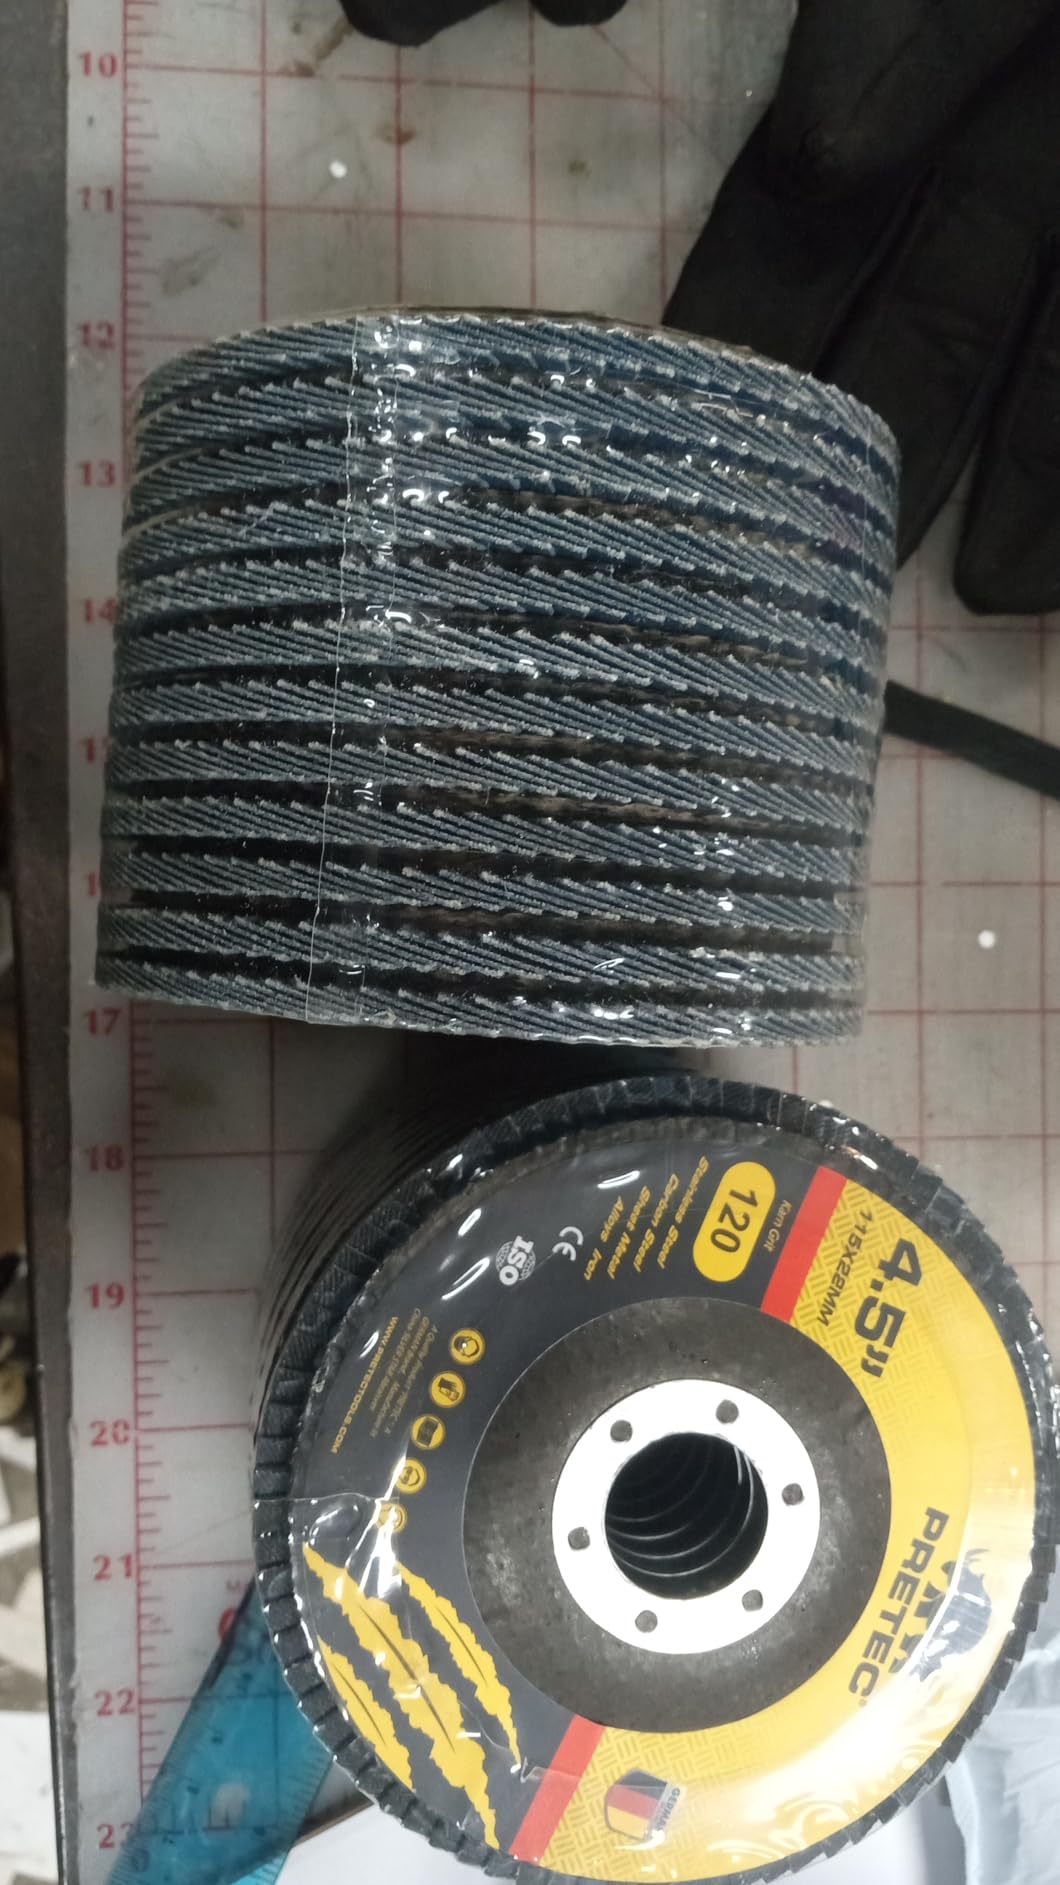
The high density zirconia held its edge through a full plate weld and the fiberglass backing plate kept the surface smear free, which matters more than people expect when the workpiece is going straight to powder coat.
Twelve discs in the pack and a one year warranty also make this a straightforward shelf refill for a shop that blends a lot of flat work.
Type 27 versus Type 29 in practice
Type 27 is flatter and its face presents more abrasive to the workpiece at once. That is why it blends flat surfaces evenly and why it cuts more slowly on edges and corners.
Type 29 is conical, so the edge sweeps forward as you increase the angle. That gives you control on edges, contours and the weld toe. If your work is mostly plate and butt joints, Type 27 is the correct geometry and most people buy the wrong one.
Where it falls short
The shallow bevel is a real limitation on inside corners and on a heavy fillet, where you need the edge to reach into the joint. This disc will not get there.
And a 60 grit still scratches. If the part is going to primer, plan a follow-up pass with a fine disc or a blending pad. Owners consistently note that the surface needs a second step.
5. SALI 60 Grit Type 29 Flap Discs – Best for Mixed Materials
Sali 10 Pack Flap Disc 60 Grit 4.5″ x 7/8-Inch Sanding Disc Bevel Type #29 Premium and Industrial Angle Grinder Grinding Wheel High Performance Edge Grinding
Grit: 60 coarse
Abrasive: zirconia alumina
Size: 4.5 inch with 7/8 inch arbor
Type: 29, 13300 RPM
Pros
- Aggressive coarse removal on hard metals
- Type 29 bevel handles contours and radius work
- Works on rust paint stainless and non-ferrous metals
- Backing plate absorbs vibration without contaminating
Cons
- Pack count is inconsistent between title and specifications
- Coarse 60 grit needs a finer follow up disc
Repair shops rarely grind one material. The same bench handles a rusted handrail, a stainless bracket and a painted frame in the same week, and this is the disc that covers all three without a separate abrasive order.
On hard metals the 60 grit zirconia alumina is properly aggressive, and the Type 29 bevel gives it the angle range to work a contour or a radius as well as a flat bead. We ground a rusty bracket down to bright metal and then took a coating line down on the same disc without a change in technique.
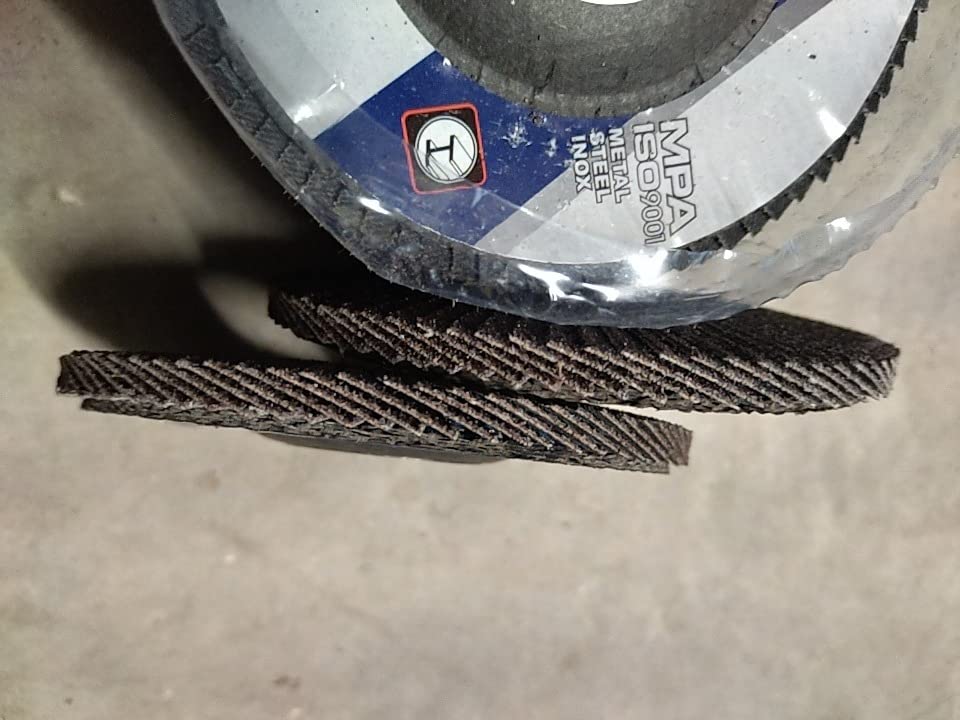
Stainless and non-ferrous metals are listed as compatible materials. That said, on stainless we would still confirm contaminant free construction before running a disc that has touched carbon steel, because compatibility is not the same as contamination control.
The rated speed is 13300 RPM, matching the grinder class we tested, and the resin fiber with fiberglass backing kept vibration down on the longer passes.
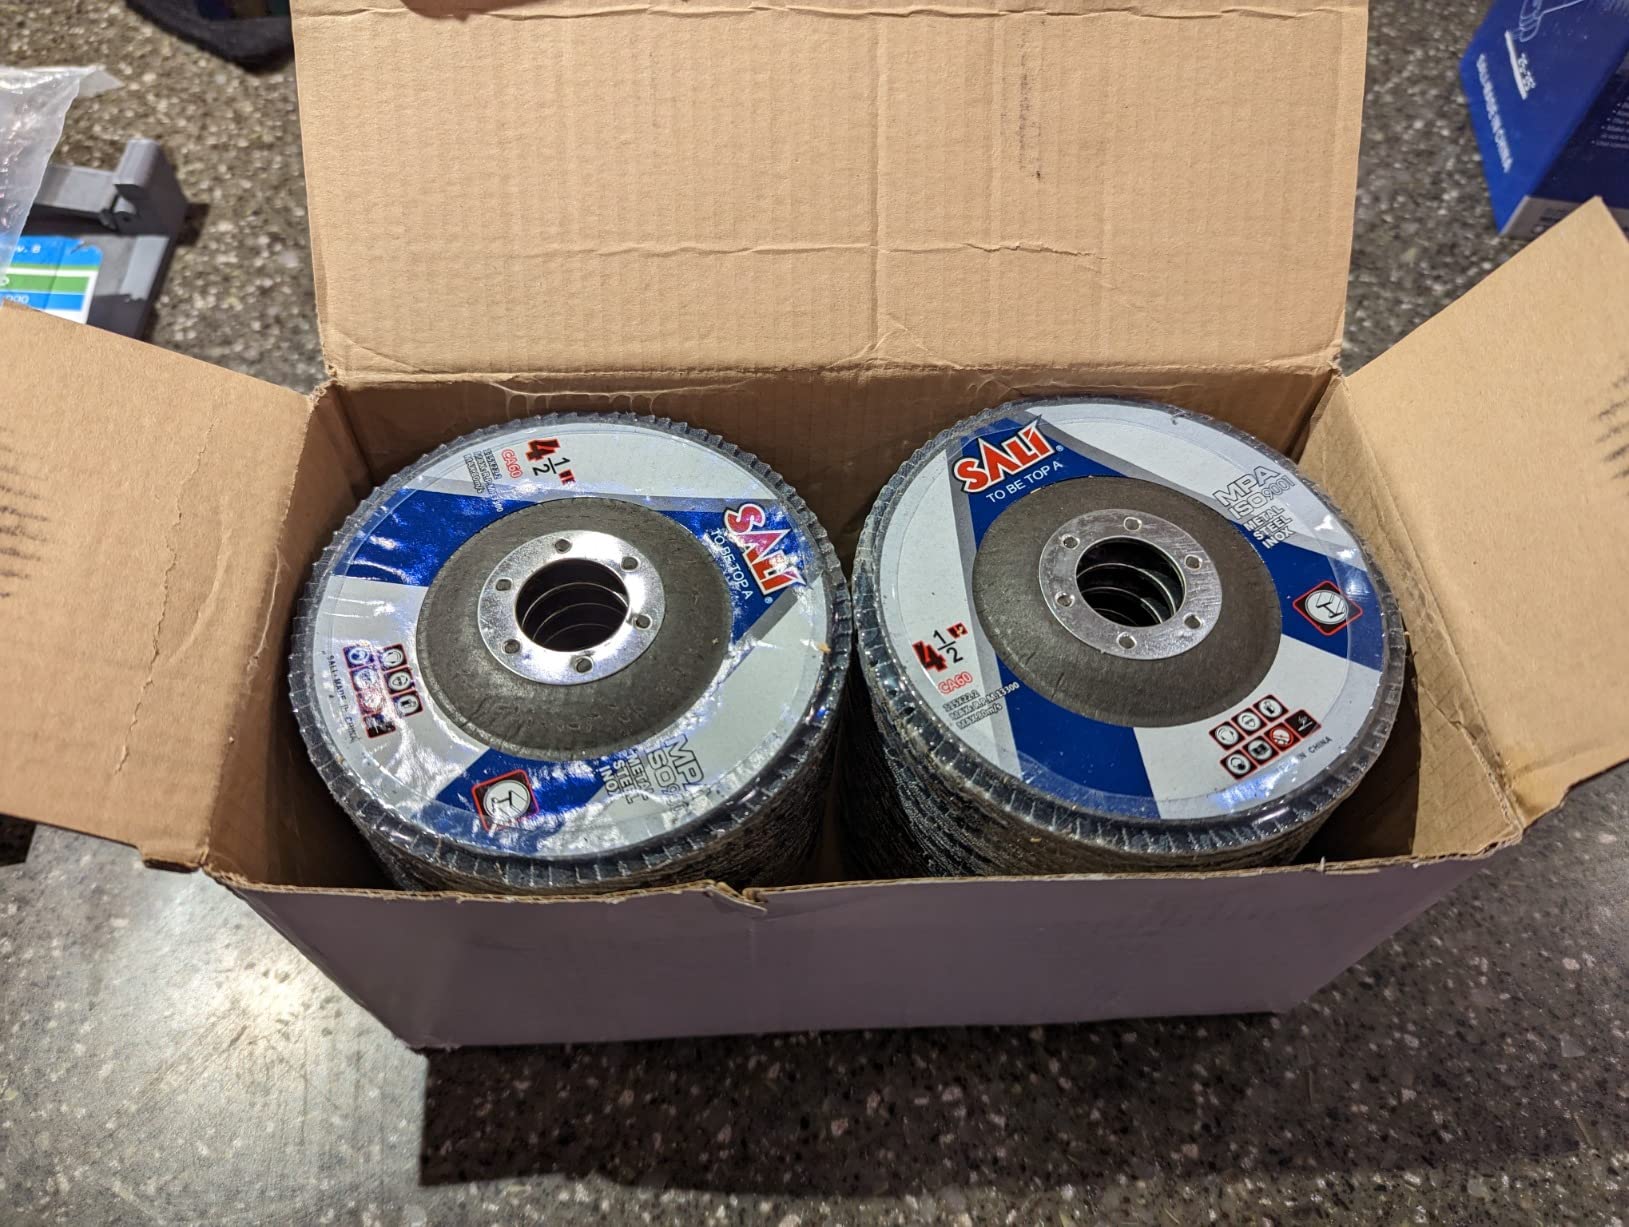
Check the pack count before you order
The listing is inconsistent about quantity, with the title and the structured specifications describing the pack differently. Owners report the same mismatch. If exact count matters for a shop budget, confirm what is in the box when it arrives.
Our advice is to treat it as a maintenance consumable and order accordingly, then count what you actually have before setting up a recurring order.
Where it is not the right tool
It is a coarse disc, so it cannot deliver the uniform matte finish a paint job needs. Plan a 120 grit or blending step behind it every time.
It is also a flat 4.5 inch disc, which means tight interior corners and fillet toes stay out of reach. For those jobs the curved radial profile is worth the extra cost.
6. PFERD POLIFAN Curve Flap Disc – Best for Fillet Welds and Inside Corners
PFERD Tools POLIFAN®-Curve Ceramic Oxide Flap Disc, 4-1/2″x 5/8-11, 60 Grit
Grit: 60 coarse
Abrasive: ceramic oxide
Size: 4.5 inch with 5/8-11 arbor
Type: radial curve, 13300 RPM
Pros
- 280 degree radial surface reaches fillet welds
- Grinds top side and bottom of a fillet in one pass
- Ceramic oxide resists thermal damage to the workpiece
- Far fewer disc flips during weld cleanup
Cons
- Threaded arbor will not fit a standard 7/8 inch grinder
- Sold as a single disc
- Not suited to flat surface or edge grinding
Every flat disc in this roundup shares one weakness, and this one is built specifically to fix it. The POLIFAN Curve uses a radial construction with 280 degrees of abrasive flap surface, so it wraps around the joint and reaches the top, the side and the bottom of a fillet without you flipping the grinder over.
On an inside corner joint that difference is night and day. With a Type 27 or Type 29 disc you are left flipping the tool three times and still missing the toe of the weld. With this disc you roll it around the corner in one continuous motion.
The ceramic oxide grain is the other reason to want it on stainless. It resists thermal damage to the workpiece, which is exactly the failure mode that leaves heat tint and a rejected part on thin stainless welds.
Why the threaded arbor matters before you buy
This disc has a threaded 5/8-11 hub rather than a collared 7/8 inch bore. That is a genuine fitment difference, not a detail to skim. A standard 4.5 inch angle grinder with a 7/8 inch arbor will not take this disc without an adapter.
Confirm your grinder before ordering, because this is the single most common reason a buyer ends up with a disc that will not mount.
When a flat disc is the better buy
If your work is plate, sheet or flat bar, this curved geometry buys you nothing and the higher per disc cost is wasted. A flat Type 29 disc will blend a butt weld faster and cheaper.
It is also sold as a single disc, which is easy to misread as a multipack at a glance. Budget for buying several if fillet weld work is a regular part of your week.
7. Sbestily 2 Inch Mixed Curved Flap Disc Kit – Best Die Grinder Corner Kit
Sbestily 13PC Mixed Curved Flap Disc 2 Inch Die Grinder Sanding Discs Kit
Grit: 40 60 80 120 mix
Abrasive: zirconia in ceramic bond
Size: 2 inch
Type: R quick change with mandrel
Pros
- Curved profile reaches welds a 4.5 inch disc cannot
- Four grit mix covers removal through final scuffing
- Included quarter inch shank mandrel adds tool compatibility
- Owners report saving a reweld by grinding a poor bead
Cons
- Grit dulls quickly on rounded corners
- Small diameter is slower on open surfaces
- Still too large for truly confined spaces
A 4.5 inch disc simply will not enter a tight bracket or the inside of a small assembly. A 2 inch curved disc on a die grinder will, and the curved profile lifts the edge off the corner so the contact area is larger than the raw diameter suggests.
The mixed grit pack is the reason this one is easy to recommend. You get 40, 60, 80 and 120 in a single kit, which means the whole ladder for small weld cleanup without ordering four separate packs and tracking four separate supplies.
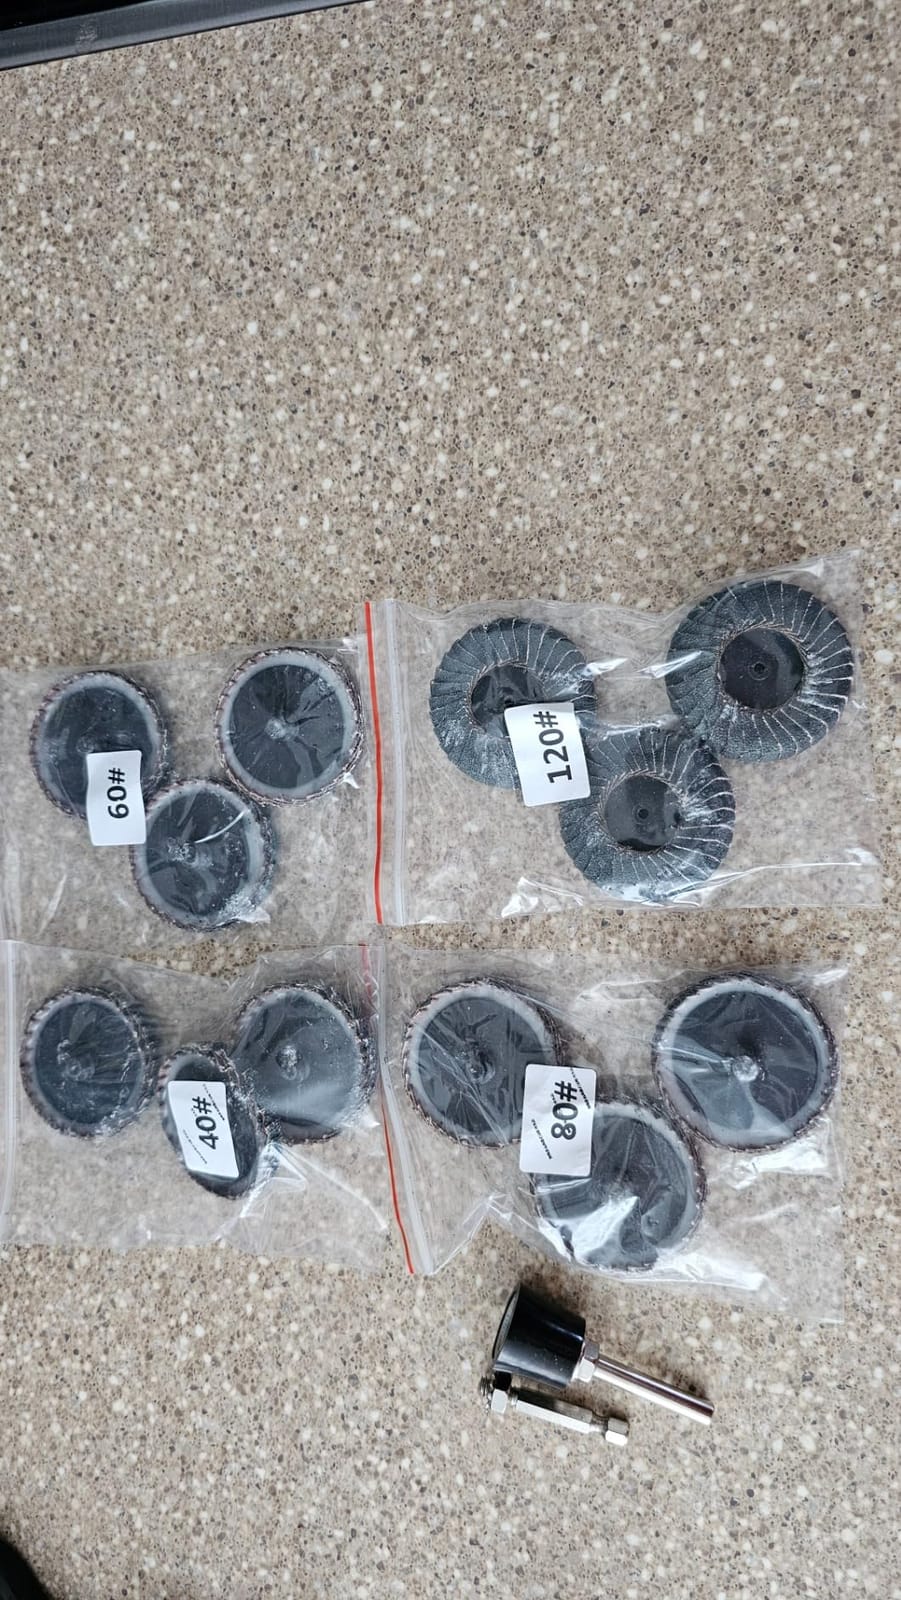
The included quarter inch shank mandrel is a genuinely useful addition. It means the discs work on a collet tool that has no quick change head, which covers a lot of older pneumatic die grinders still sitting in repair shops.
One user story stood out in the reviews. Someone ground down a poorly set bead rather than reweld the joint, which is the real economics argument for owning a small curved disc. Saving a weld on a bracket is worth more than a year of disc costs.
Grinding corners versus grinding flat plate
On a rounded corner the disc spends its life on the edge of the disc rather than the face, and edges are where flaps thin out and dull fastest. Owners report the corner grit stops cutting noticeably before the face is finished.
Rotate the disc a quarter turn when the edge goes first. It buys real extra time on a corner-heavy job, and it costs nothing.
Where it loses to a big disc
Open surface work. A 2 inch face simply moves less metal per pass than a 4.5 inch face, and on a long seam in the open the big disc is faster by a wide margin. Use the two inch for access, not for throughput.
Also note the honest limit: small diameter is not the same as deep access. If the constraint is how far your hand can reach rather than the width of the opening, no disc in this roundup solves it.
8. Benchmark Abrasives 2 Inch Quick Change Flap Discs – Best for High-Speed Die Grinders
Benchmark Abrasives 2″ Quick Change Zirconia Flap Disc Grinding Wheel with Male R-Type Back Design – Cleaning Finishing Deburring of Irregular Surfaces – for Die Grinder & More (10 Pack), 36 Grit
Grit: 36 coarse
Abrasive: zirconia
Size: 2 inch
Type: R quick change, 24000 RPM
Pros
- Two inch face reaches narrow and hard to reach areas
- 36 grit zirconia cuts fast on weld lines and splatter
- Quick change back locks straight into the collet
- Rated to 24000 RPM for pneumatic die grinders
Cons
- Small face slows heavy open surface material removal
- Access depth rather than diameter still limits some spots
This is the one to buy if your die grinder runs fast. The 24000 RPM rating is the highest in this roundup and it covers the pneumatic die grinders and high speed electric tools that the 2 inch curved kits in this category are often not rated for.
The 36 grit zirconia is the coarsest abrasive here, which is right for the job this disc actually does. Weld splatter and the base of a bead are hard, dirty work, and a coarse grain with fast zirconia removes it without the disc bogging down.
The male R type quick change back locks directly into the die grinder collet, so disc changes take seconds. On a job with several brackets to clean up, that convenience matters more than it sounds.
Fit is broad across the major die grinder brands, and the discs are built to exceed ANSI and EU standards for abrasive products, which is the certification mark we look for on anything spinning at this speed.
Rating the RPM honestly
Every disc has a printed maximum speed and that number is a hard limit, not a guideline. Running a disc above its rating risks the abrasive failing at speed, and the failure mode at die grinder speeds is violent.
Match the disc rating to the tool rating and never exceed either. If your tool is rated above 24000 RPM, this disc is still safe because it is rated lower, but do not assume a lower rated disc can be run faster than its marking.
Where it falls short
Open surfaces again. The small face is the trade for the access, and on a long seam in the open a 4.5 inch disc will move material faster every time.
The rating in this group is also a notch below the 4.5 inch discs, and the feedback reflects that, with the small diameter cited as the recurring limitation. Judge it as a detail tool, which is exactly what it is.
9. 3M Grind Less Weld More Kit – Best All-In-One Weld Finishing System
3M Grind Less Weld More Promo Kit, 67115
Contents: 16 pieces at 4.5 inch
Includes fibre flap grinding cut off blending strip
Back-up pad included
Cubitron 3 and Scotch-Brite
Pros
- Covers a full weld cleanup workflow in one purchase
- Cubitron 3 fibre discs cut faster than the prior generation
- Clean and Strip XT Pro removes rust paint and mill scale
- Back-up pad included so nothing else is needed
Cons
- Costs more than a single specialty disc for one job
- Only two flap discs in the kit
- Marked for industrial and occupational use only
This is the honest answer to a question most roundups avoid. Some weld cleanup jobs are not better with a better flap disc. They are better with a fibre disc, a blending pad and a strip disc, because those steps are what actually take a weld to a paint ready surface.
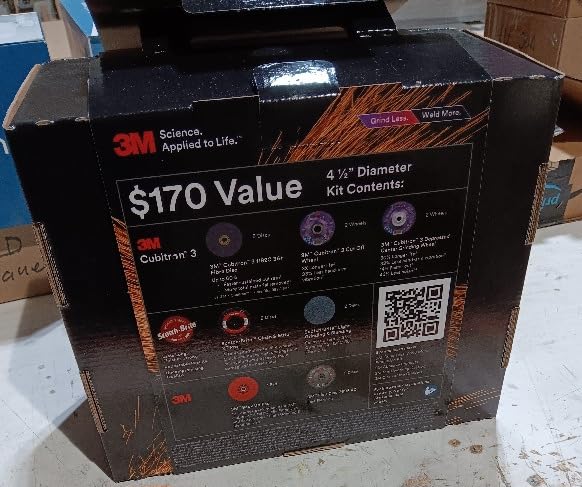
The kit is 16 pieces at 4.5 inch and it covers that whole sequence: fibre discs, quick change flap discs, grinding wheels, cut off wheels, blending discs, strip discs and a ribbed back-up pad. Owners describe it as the easiest way to sample the Cubitron and Scotch-Brite range before committing to a bulk order.
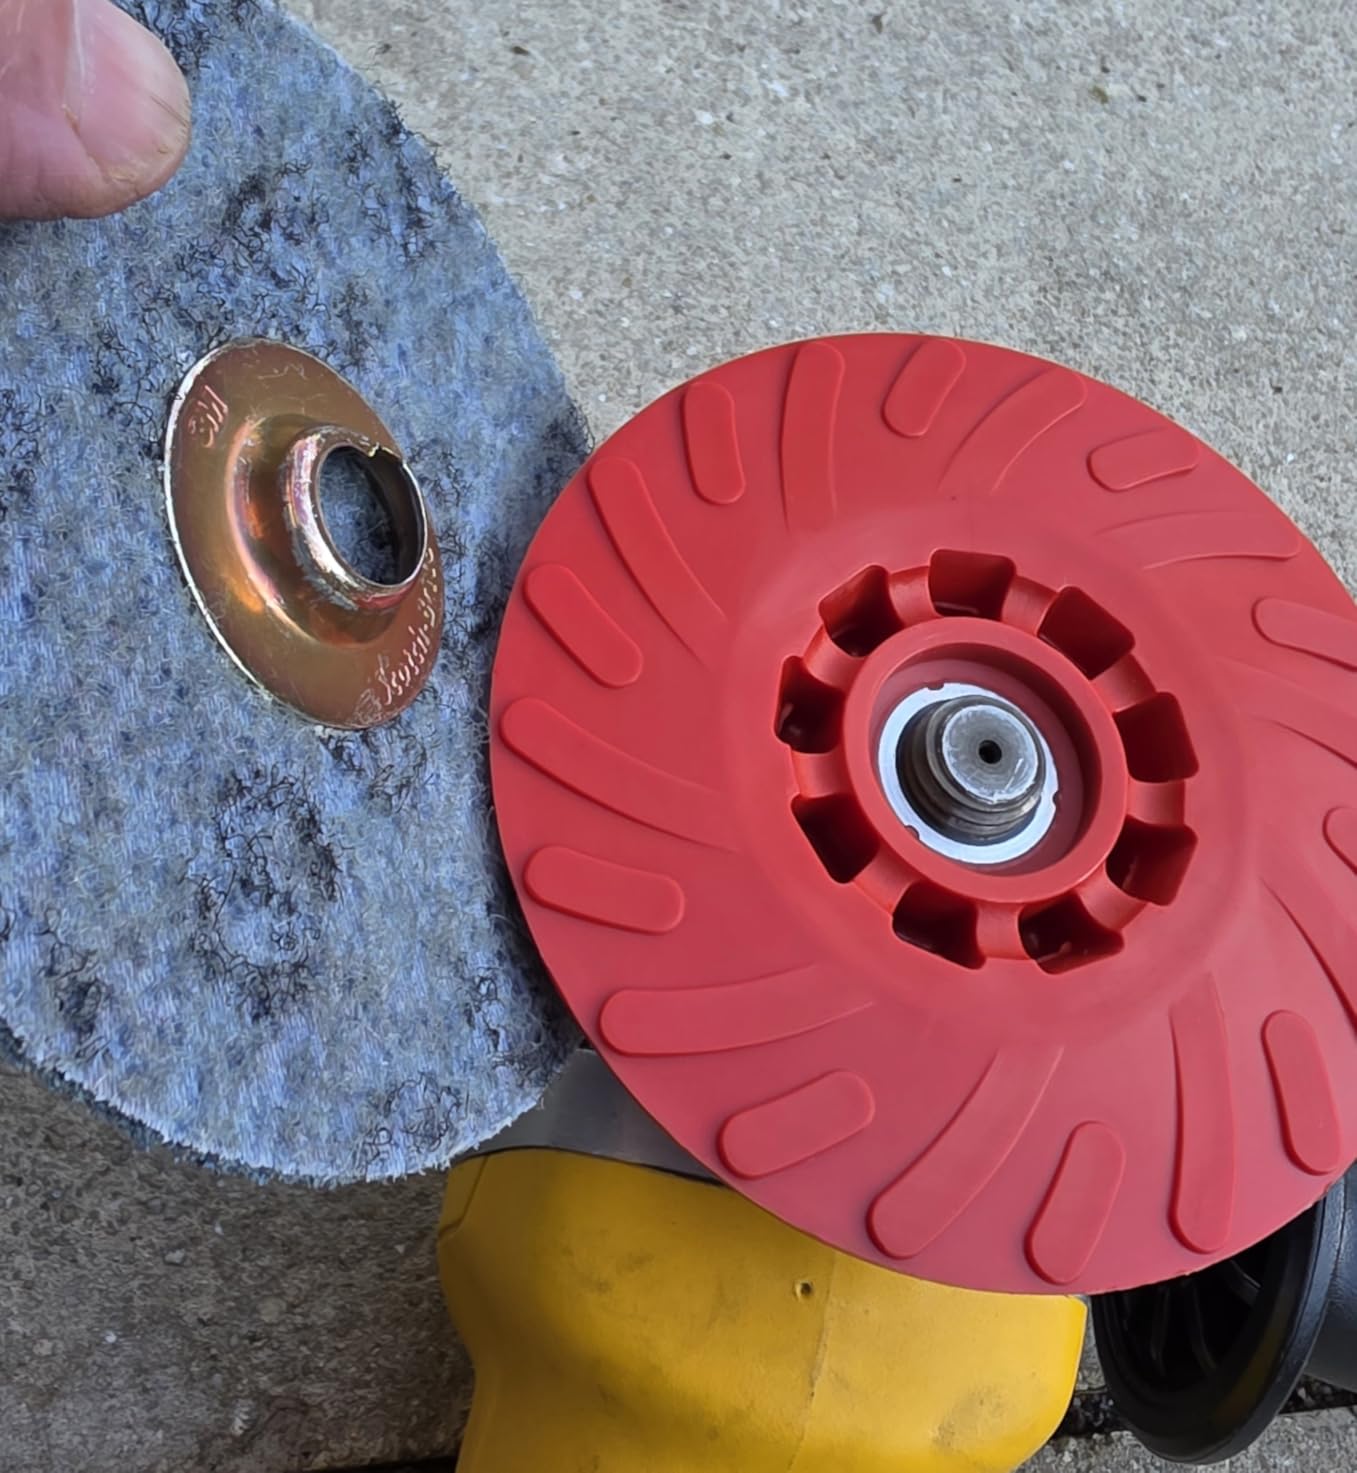
Two specifications stand out. The Cubitron 3 1182C fibre discs claim up to 51 percent faster initial cut and 61 percent faster sustained cut than the previous generation, and the Scotch-Brite Clean and Strip XT Pro discs strip rust, paint and mill scale without the loading a coated abrasive suffers.
That two step system is the real lesson here. Fibre disc first to remove the bulk, then a blending disc to finish. Several fabricators on welding forums report reaching for fibre discs over flap wheels for heavy removal for exactly this reason.
When a kit beats buying one disc at a time
A kit wins when you do varied work. One disc type solves one problem, so a shop that grinds, blends, strips and deburrs needs at least four abrasive types anyway, and the kit gets you all of them plus the back-up pad in one order.
A kit loses when you have one specific problem. If you only blend 40 grit welds on plate, a single high density flap disc pack serves you better and costs less.
Watch the contents before you commit
There are five fibre discs and only two of each other type, so in heavy use the fibre discs run out first. Plan on replacing those first.
It is also marked for industrial and occupational use only, so check that wording against how you work. And note the included flap discs are 40 grit Type 27 quick change, which covers roughing but not your finishing step.
10. Trivd Frol 40 Piece Mixed Grit Pack – Best for a Full Grit Ladder
40 Pack Flap Discs 4 1/2 for Angle Grinder Sanding Disc – Trivd Frol 40/60/80/120 Grit T29 Flap Disc, 7/8 Inch Zirconia Abrasive Grinding Wheel Disc for Metal, Wood, Stainless Steel Finishing
Contents: 40 pieces at 4.5 inch
Grit mix from 40 to 120
Abrasive: zirconia
Type: 29, 13300 RPM
Pros
- One pack covers the whole grit ladder
- Zirconia runs cool and resists smearing
- Fiberglass backing absorbs vibration
- Strong value per disc for high volume shops
Cons
- Grit split is weighted heavily toward 40 grit
- Not for concrete or stone grinding
If your complaint is that you never seem to have the right grit on the shelf, this pack ends the problem. Forty discs at 4.5 inch split across 40, 60, 80 and 120 grit, so a complete ladder is always available without a second order.
The Type 29 zirconia discs handle the range of work we threw at them: light rust removal, deburring, weld grinding, blending and finishing on steel, alloyed steel, composites, plastics and wood. The 13300 RPM rating and the reduced friction heat design showed up in practice as a cooler cut and less smearing on the workpiece.
For a shop or a serious hobbyist grinding every week, the per disc economics of buying this much abrasive in one order is the argument. High volume buyers specifically call out not having to reorder constantly.
The fiberglass backing plate is the same vibration absorbing construction used across the better discs in this roundup, and it is why the surface came off clean rather than smeared.
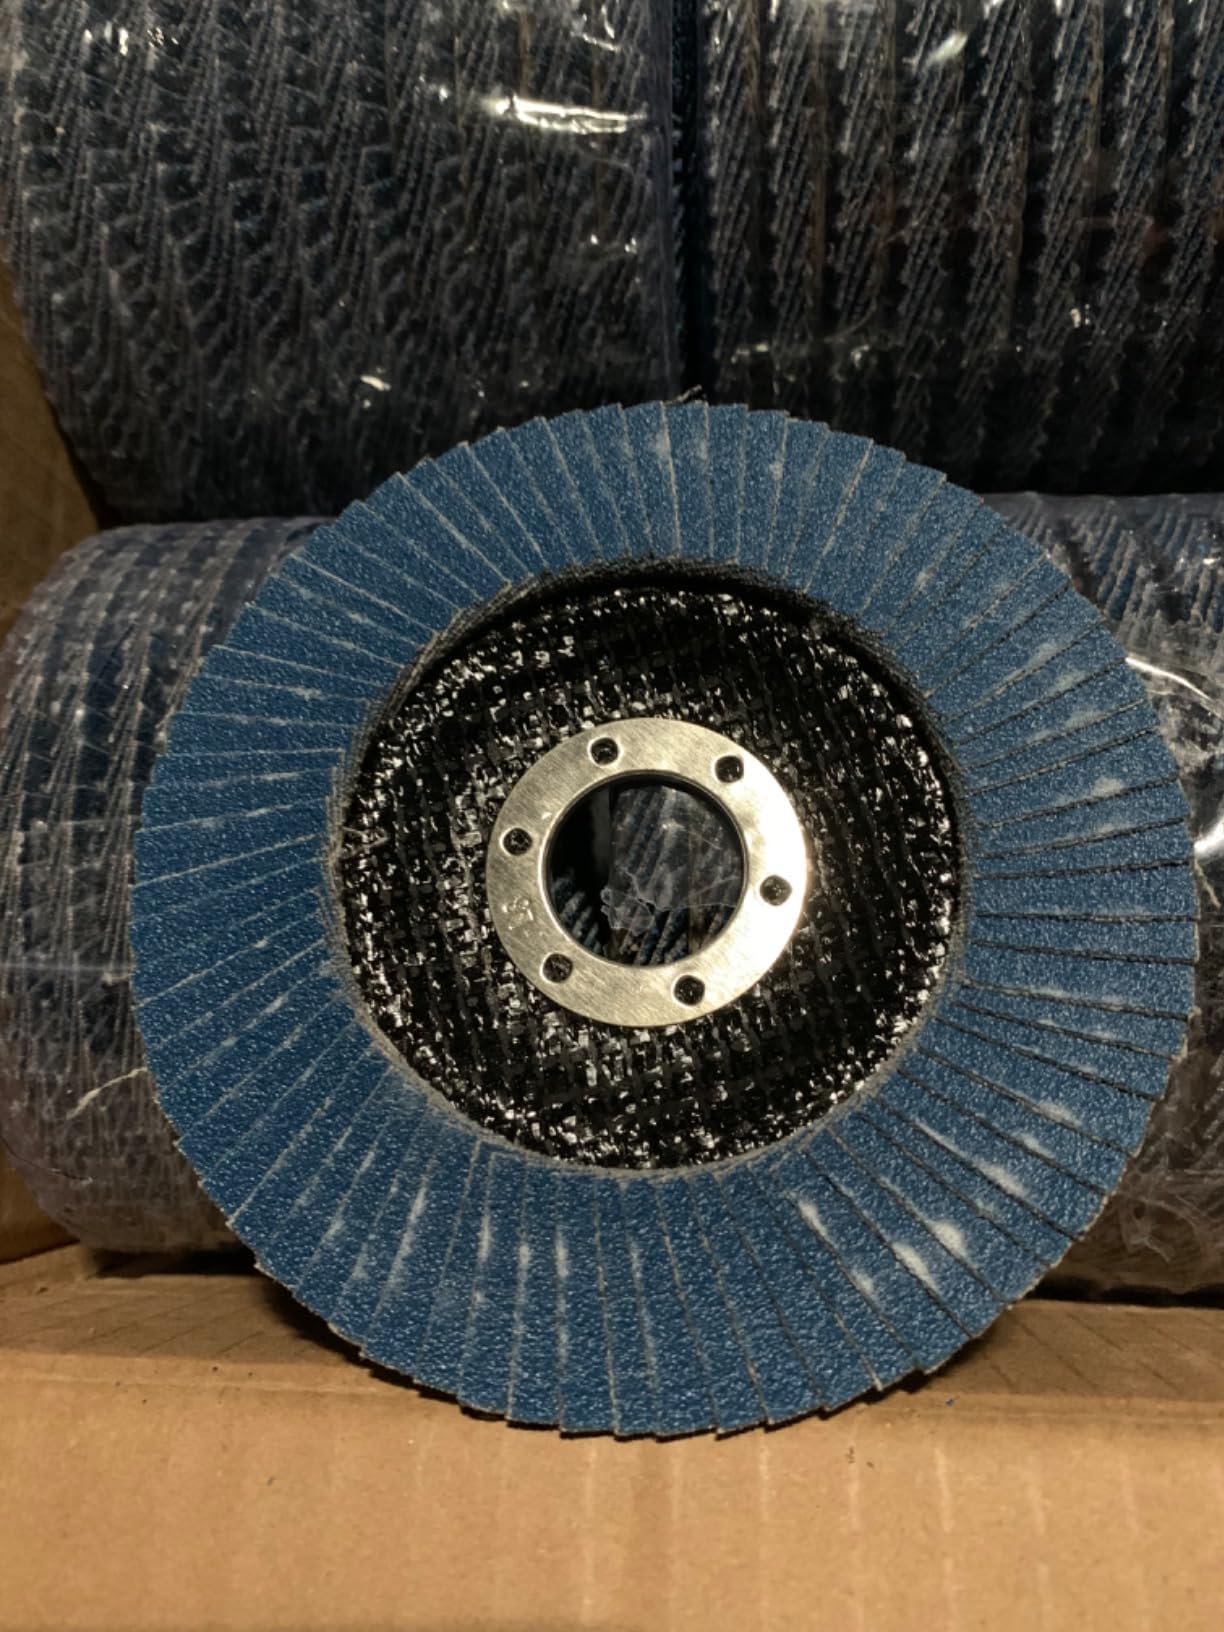
Reading the grit split before you rely on it
The distribution is weighted toward coarse: twenty pieces at 40 grit, ten at 60, five at 80 and five at 120. If you are doing mostly finish work, the fine end of the ladder will run down first and you will top it up separately.
Be aware too that the structured listing field names 40 grit while the set includes four grits, so the metadata is inconsistent even though the physical contents are a mixed pack.
When one disc type is still the answer
If your grinding is mostly flat plate and butt welds, a dedicated 40 grit pack will serve you better and you will not be tempted to use a coarse disc for finishing.
And it is explicitly not for concrete or stone. On masonry work you want a different abrasive entirely, and no amount of zirconia changes that.
Flap Disc vs Fibre Disc vs Grinding Wheel: Which One for Which Step
The fastest way to waste shop time is reaching for the wrong disc. A grinding wheel, a fibre disc and a flap disc all remove metal, but they occupy different steps in a weld cleanup sequence and mixing them up costs you time and finish quality.
Start with a depressed center grinding wheel or a coarse fibre disc when the reinforcement is genuinely proud, meaning multiple passes or heavy multipass weld standing well above the plate. These cut the fastest and will take the bead down to near flush in a fraction of the time, but they leave deep parallel scratches and round the edges of the plate.
Move to a coarse flap disc at 40 grit once the bead is close to flush. This is where the flap construction earns its keep, blending the weld into the surrounding plate instead of cutting a groove across it.
Finish with a 60 or 80 grit flap disc to knock down the 40 grit pattern, then a 120 grit flap disc or a blending pad for the uniform matte surface that will hold primer. Owners who skip this step are the ones whose welds telegraph through paint.
A fibre disc sits between the grinding wheel and the flap disc in this sequence. It removes material faster than a flap disc and leaves a slightly better surface, which is why the 3M kit in this roundup leads with fibre discs for heavy work and blending discs for the finish.
One piece of practical wisdom from fabricators deserves repeating here. On heavy production pipe weld cleanup, many shop owners argue that grinding by hand is a waste of time and that the weld should go to a machine. On a one-off or a repair, the ladder above is the right call. On production, cap your expectations and price the time accordingly.
How to Buy the Right Flap Disc for Weld Cleanup
Match the arbor before anything else, because it is the only mistake that makes a disc useless. Most 4.5 inch angle grinders use a 7/8 inch arbor with a raised collar, and every 4.5 inch disc in this roundup except the PFERD uses that fit. The PFERD uses a threaded 5/8-11 hub and needs a matching grinder or an adapter.
Die grinder discs are a separate system entirely. The 2 inch curved discs in this roundup use an R type quick change attachment that locks into the collet, and some kits include a quarter inch shank mandrel for tools without a quick change head.
Check the rated speed next. All of the 4.5 inch discs here are rated to 13300 RPM, and the 2 inch Benchmark die grinder disc is rated to 24000 RPM. Match the disc rating to your tool and never run above the marking.
On grit, the ladder is simple and it does not change by brand. Forty for gouging reinforcement and heavy spatter, sixty for blending the weld into the plate, eighty for knocking down the scratch pattern, and one hundred twenty for a paint ready finish.
On grain, match the work to the load. Aluminum oxide is fine for occasional hobby touch-ups on clean mild steel. Zirconia is the default for carbon and stainless steel because it resists glazing. Ceramic grain is worth it on stainless, on thin wall where heat matters, and on production work where cut rate per minute is what pays.
On geometry, the rule we use is simple. Flat plate and butt welds get a Type 27 for its broader contact patch. Edges, contours and weld toes get a Type 29 for its forward-raked edge. Inside fillet corners get a curved radial disc.
On stainless and aluminum, ask about contamination rather than assuming. A disc that has touched carbon steel can leave iron behind that rusts later as a bloom along the blended area. Look for a stated contaminant threshold or a product line documented for stainless use, and keep stainless discs separate from carbon steel discs rather than wiping them off and reusing them.
On density, remember that more abrasive behind the face means a longer working life and a more even scratch pattern. That is the main reason to pay more per disc, and it is the reason shop owners buy the high density discs by the box.
Finally, buy for the grit you actually use. A shop that grinds daily burns through 40 grit and barely touches 120 grit, so a coarse-heavy pack is correct. A shop doing finish work needs the opposite balance. The mixed packs in this roundup are a reasonable hedge when you are not sure yet.
One housekeeping note for anyone grinding indoors. Abrasive dust is fine and it settles into welds and equipment fast, so a shop vacuum around the bench pays for itself. Our picks for keeping up with that kind of debris are covered in our guides to the best cordless stick vacuums for quick cleanups and the best cordless leaf blowers for fall cleanup, either of which will clear a bench faster than a broom.
How to Get More Life Out of a Flap Disc
Watch the angle of attack. A disc held nearly flat works its whole face and spreads the load evenly. Tilting the disc too far forward concentrates the work on the edge, where the flaps are thinnest, and that edge will dull long before the face is spent.
Let the disc warm before you work. A cold disc on cold steel grabs and chatters. Bring it up to speed against the work for a moment before you add pressure and you will get a cleaner cut and a longer life.
Rotate when the edge goes. On corner and edge work, turning the disc a quarter turn puts fresh face material into the job. It takes seconds and it is the difference between one pass and three.
Change grits instead of forcing a worn disc. A glazed 40 grit does not cut, it burnishes, and burnishing makes the primer adhesion worse rather than better. When the cut rate drops noticeably, move to a fresh disc rather than leaning harder.
Clean the flaps when they load. A disc that picks up weld spatter or coating residue stops cutting and starts rubbing. A stiff brush across the face between passes restores the cut and costs nothing.
Finally, learn the wear indicators on the discs you buy. Some quality discs include printed arrows or marks that show remaining life, which tells you when the disc is done instead of leaving you to guess. On the rest, the practical rule is simple: when the flaps are worn to the rivets and the face is down to the backing, it goes in the scrap bin, not back on the grinder.
Frequently Asked Questions
What is a flap disc used for?
A flap disc is a layered abrasive disc whose overlapping sandpaper flaps wear away during use to expose fresh grain. That lets a welder grind down a weld bead, blend it flush with the surrounding steel, deburr an edge and prep the surface for paint in a single step with one tool, without the deep parallel scratches a grinding wheel leaves behind.
What grit flap disc is best for welds?
Start at 40 grit to remove weld reinforcement and spatter, move to 60 grit to blend the weld into the plate, then 80 or 120 grit to knock down the scratch pattern and leave a uniform matte surface that will hold primer. Going straight to a fine grit wastes time on heavy reinforcement and never removes it evenly.
What are the differences between a 40 grit and a 60 grit flap disc?
A 40 grit is a roughing disc. It removes proud reinforcement, spatter and heavy mill scale quickly and leaves a deep scratch pattern. A 60 grit removes far less material per pass and is used to blend the weld into the base metal once the bead is close to flush. The 40 grit is for removing metal, the 60 grit is for blending it.
What are the differences between aluminum oxide and zirconia flap discs?
Aluminum oxide is the economical baseline grain. It works fine on clean mild steel for light work but glazes quickly under sustained load. Zirconia is a tougher grain that holds its edge on steel, stainless and cast iron, which makes it the sensible default for weld cleanup. Ceramic grain cuts fastest and runs coolest, and earns its cost on thin stainless where heat tint is a defect.
What is the best disc to use for grinding down welds?
Use a grinding wheel or coarse fibre disc first when the reinforcement stands well proud of the plate, then switch to a 40 grit flap disc to blend it flush, then a 60 to 120 grit flap disc for the finish. The grinding wheel is fastest for removing metal and the flap disc is faster for blending it, so the sequence beats trying to do both jobs with one disc.
What grit flap disc for welding prep before paint or powder coat?
End on 80 or 120 grit. Blend the weld at 40, level it at 60, then take a finishing pass at 80 or 120 until the whole blended area reads as one even matte surface. A coarse scratch pattern will still telegraph through primer or powder coat, which is why the fine final step is the one people skip and regret.
Do flap discs work on aluminum and stainless steel?
Yes, but pick the disc for the job. On aluminum use a fine to medium grit because coarse discs gouge soft metal and can gum up, and confirm the disc is suited to non-ferrous work. On stainless, choose a ceramic or documented stainless line and keep it separate from carbon steel discs, because iron contamination left by a carbon steel disc causes after-rust along the blended area.
Type 27 or Type 29 for weld cleanup?
Type 27 is nearly flat and is worked at a shallow 5 to 15 degree angle, giving a broad even contact patch that blends flat plate and butt welds nicely. Type 29 is conical and is worked at 15 to 20 degrees, raking the edge forward for control on edges, contours and weld toes. For inside fillet corners, choose a curved radial disc instead of either.
What do I use for inside fillet welds and tight corners?
Use a curved radial flap disc. A flat Type 27 or Type 29 disc cannot reach the bottom of an inside corner no matter how you hold the grinder, so you end up flipping the tool repeatedly and still missing the toe of the weld. A curved disc wraps 280 degrees or more around the joint and cleans the top, side and bottom in one continuous motion.
Why is my flap disc digging into the metal instead of cutting?
Usually one of four things: the disc is glazed and worn, the angle of attack is too steep so the edge digs instead of the face working, you are pressing too hard so the disc has nowhere to go, or you are on thin wall and the grit is too coarse for the material. Start with a fresh disc, hold it flatter, let the grinder weight do the work, and step the grit down.
Final Verdict on the Best Flap Discs for Weld Cleanup
For most welders the answer is simple. Buy a 40 grit zirconia Type 29 for roughing and blending, keep a 60 grit on the shelf for leveling the blend, and finish every weld at 120 grit. The EZARC carries that combination and has the largest review base of any disc in this roundup, which makes it our starting point.
Add a curved radial disc if you weld inside corners, and check the arbor before you order because a threaded hub will not fit a standard grinder. Shop owners grinding daily should step up to the high density Benchmark discs for wear life, and anyone doing varied work should look at the 3M kit rather than buying one abrasive type at a time.
Whichever you choose, respect the rated speed, keep the guard on, and step the grit ladder rather than leaning harder. That habit alone will outlast any brand decision you make today.